The Working Principle of Automatic EVA Sole Washing Machine in Footwear Production
The Core Task: Why EVA Soles Need Automated Cleaning
EVA (ethylene vinyl acetate) foam soles present a unique cleaning challenge. The material is porous, with a low density and interconnected open-cell structure that allows oils and mold release agents to penetrate deep into the foam-not just sit on the surface. Before any gluing, painting, or UV treatment can succeed, these contaminants must be completely removed.
Traditional methods have relied on manual roughening or solvent wiping with toluene and benzene derivatives. Both approaches are problematic: manual roughening is labor-intensive and inconsistent, while organic solvents are toxic, can accumulate in the bloodstream, and pose long-term occupational health risks . Automatic EVA sole washing machines were developed to replace these methods with a closed, repeatable process that delivers consistent cleaning quality at production scale.
Understanding how these machines work requires examining their mechanical architecture, the cleaning chemistry they employ, and the sequence of actions that takes a contaminated sole to a bonding-ready surface.
The Mechanical Architecture: Two Major Configurations
Automatic EVA sole washing machines in footwear production fall into two broad categories based on how they move soles through the cleaning stages. Each has distinct mechanical principles.
Batch Rotational Design
One established design uses a rotary cleaning frame that dips into and out of a cleaning bath. The machine consists of an electric cabinet and a main cabinet body housing a hydraulic cylinder, an AC variable-frequency motor, and a rotary lifting shaft .
The cleaning frame itself is a circular barrel made of 304 stainless steel, with a large number of round holes on its sides and bottom. Soles are loaded into this frame, which is mounted on the rotary lifting shaft. The frame's movement follows a defined trajectory: it slowly descends into the storage tank containing the cleaning solution, rotates at low speed in both forward and reverse directions for several seconds each, then rises slowly. Once the frame bottom clears the liquid surface, the motor accelerates to high speed for a few seconds, using centrifugal force to spin-dry the cleaning solution from the soles. The frame then stops rotating and continues its ascent to the viewing window position .
The rotational speed during cleaning is kept below 100 rpm, with a cycle time of 2–5 minutes. The lifting speed reaches up to 10 meters per minute . This design is compact and fits production areas with limited floor space.
Continuous Conveyor Design
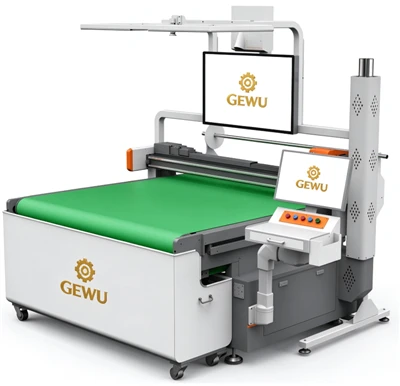
The more common configuration in high-volume footwear production uses a continuous conveyor system. Soles are carried through a series of treatment stations on upper and lower mesh belts that clamp them in place. The upper belt incorporates a crank mechanism that automatically adjusts to different sole thicknesses, accommodating various midsole and outsole dimensions without manual changeover .
This conveyor-based design integrates multiple processing stages in sequence: an ultrasonic cleaning tank, a rinse section with high-pressure spray nozzles, a neutralization tank, and a drying chamber. The continuous flow allows for throughput rates of 700–1,200 pairs per hour depending on configuration .
The Cleaning Sequence: From Contaminated to Bonding-Ready
An automatic EVA sole washing machine does not simply wash soles-it executes a defined chemical and mechanical sequence designed to prepare the surface for adhesion. The process typically follows these stages.
Stage 1: Ultrasonic Cleaning and Chemical Treatment
The first stage is the most critical for removing mold release agents and oils. Soles enter a treatment tank containing a heated acidic solution. For EVA material specifically, the tank temperature is maintained at 50–60°C-lower than the 65–75°C used for rubber, because EVA foam is more heat-sensitive and can deform at higher temperatures .
The treatment solution includes a surfactant and corrosion inhibitor, with the pH adjusted to an acidic range (typically pH 2.0–2.5). This acidic environment helps break down oils and release agents .
Simultaneously, ultrasonic transducers mounted beneath the tank generate high-frequency mechanical oscillation. At a frequency of 28 kHz, this oscillation creates microscopic bubbles in the solution. When these bubbles collapse near the EVA surface-a phenomenon called cavitation-they generate intense localized energy that dislodges contaminants from within the foam's open-pore structure . The ultrasonic energy penetrates the porous EVA surface, reaching oils that have migrated below the surface layer.
Stage 2: High-Pressure Rinse
After the treatment tank, soles pass through a rinse stage where high-pressure spray nozzles flush away loosened contaminants and residual treatment solution. The spray pressure is maintained at a minimum of 0.5 kg/cm², with at least two sets of nozzles positioned to cover the full sole surface .
Water at room temperature is used for rinsing, removing the acidic solution and any remaining debris .
Stage 3: Neutralization
The third treatment stage addresses the residual acidity from the first tank. Soles enter a neutralization tank containing an alkaline solution at pH 10.5–12, maintained at 45–55°C. This step neutralizes any remaining acid and adjusts the surface chemistry to a condition suitable for primer application .
For EVA midsole processing specifically, the neutralization tank may be adjusted to pH 3–4, depending on the material and the downstream bonding requirements .
Stage 4: Drying
The final stage removes moisture from the cleaned soles. A specially designed drying chamber uses blowers and air knives to produce a high-velocity air stream that strips water from the sole surface. The chamber is designed to automatically purge vapor, and the combination of blower and air knife achieves effective drying .
In some conveyor designs, the drying stage includes a heating function for humid environments, while dry conditions may require only ventilation . The goal is a sole that exits the machine clean, neutralized, and dry-ready for immediate primer application.
Key Design Features That Enable Consistent Operation
Several engineering details distinguish a production-grade automatic EVA sole washing machine from simpler cleaning equipment.
Multi-stage chemical processing reflects the recognition that EVA cleaning requires more than a single wash. The acid-rinse-neutralize sequence ensures that oils are removed, residues are flushed, and surface chemistry is optimized for bonding .
Material compatibility controls protect the EVA foam from damage. Lower treatment temperatures for EVA compared to rubber prevent thermal deformation. The neutralization stage protects against acid residue that could degrade the foam over time .
Automated thickness adjustment in the conveyor system allows the machine to process different sole types without manual reconfiguration. The upper mesh belt's crank mechanism automatically adapts to varying sole dimensions .
Enclosed construction with stainless steel components and sealing panels contains the cleaning solution, prevents splashing, and isolates noise from blowers and air knives. This creates a safer and quieter working environment compared to manual cleaning stations .
Solution recovery systems reduce consumption and environmental impact. The storage tank is positioned to collect spun-off cleaning solution, allowing reuse and reducing waste .
Why the Automatic Process Improves on Manual Methods
The working principle of the automatic machine addresses the fundamental limitations of traditional EVA surface preparation.
Manual roughening creates a mechanical profile for adhesion but damages the foam structure and generates dust. Solvent wiping dissolves oils but introduces toxic chemicals into the workplace and depends entirely on operator technique. Neither method can reliably clean the interior of EVA's porous structure.
The automatic machine's combination of ultrasonic cavitation, heated chemical treatment, and high-pressure spray penetrates the open-cell foam and removes contaminants from within the material, not just the surface. The multi-stage process is repeatable-every sole receives the same treatment time, temperature, and chemistry. And the aqueous cleaning approach eliminates the VOC exposure and occupational health hazards of solvent-based methods .
For footwear manufacturers producing EVA-soled shoes at scale, the automatic EVA sole washing machine transforms what was once a labor-intensive, inconsistent, and hazardous manual step into a controlled, repeatable, and environmentally responsible production process.